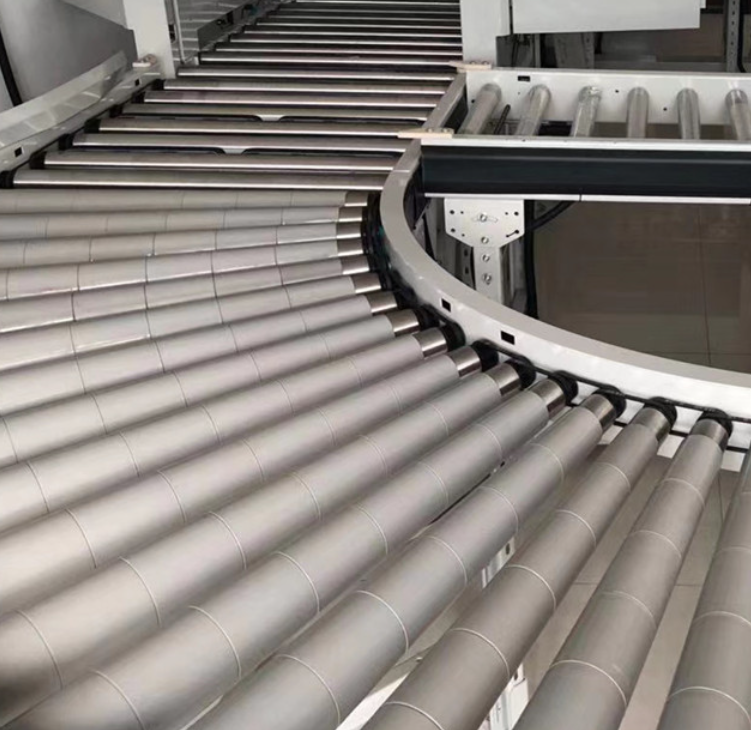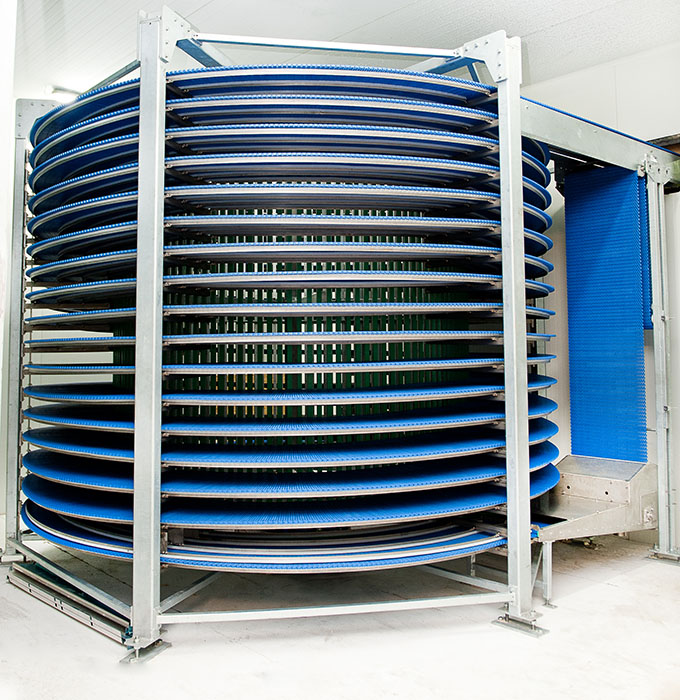
A spiral conveyor used to change line direction, move product between floors and save floor space, particularly favoured for cooling products that require IQF.
Eliminate unplanned downtime, increase efficiency and boost profitability with a spiral conveyor.
Spiral conveyors are critical equipment across many industries, particularly food processing and container manufacturing. The right spiral solution can bring efficiency to processes such as freezing and cooling; the wrong one can bring the entire line to a halt. Spiral conveyors are used to change line direction, move product between floors and save floor space. They are especially used to cool products requiring IQF, such as meat and flour-based products, and various types of bread. The belt type, width, number of tiers and diameter used are determined according to the product being conveyed and the intended application.
The Intralox modular plastic spiral conveyor belts used here minimize costly, unplanned production downtime, eliminate complex repair work, and overcome product quality and orientation challenges. Spiral conveyors are designed with hygiene in mind; they have no contamination-trapping points or small crevices, and their rod-retention areas are designed for fast, thorough cleaning.
| Technology Partner | Intralox modular plastic belt |
| Application | IQF, cooling, floor-to-floor transfer |
| Belt Configuration | Type/width/tier count/diameter selected by product and application |
| Application Areas | IQF, meat/flour-based product cooling, floor transfer |